In the food and beverage industry, water is more than a utility—it is a primary ingredient, a cleaning agent, and a critical line of defense against fire. Whether you are running a commercial bakery, a bottling plant, or a cold-storage facility, your operational success depends on the reliability and hygiene of your water storage.
As we look toward the 12th Annual Fire Systems Design & Engineering Conference this April, we are highlighting why Rainbow Reservoirs remains the preferred partner for South Africa’s leading food producers.
1. Hygiene-First Engineering
Food safety standards like HACCP and ISO 22000 require that every component of a production facility prevents contamination. Standard reservoirs can often harbor algae or allow for sediment buildup.
Rainbow Reservoirs utilizes heavy-duty, food-grade internal liners that ensure your water never comes into contact with the tank’s structural shell. These liners are:
- BPA-Free and Certified: Safe for potable water and food processing.
- Light-Proof: Preventing the photosynthesis required for algae growth.
- Water-Tight: Eliminating the risk of external contaminants seeping into the supply.
2. The Aluzinc® Advantage in Sensitive Environments
Food production often involves high humidity or the use of corrosive cleaning chemicals. Traditional galvanized steel tanks can struggle in these environments, leading to oxidation and structural weakness.
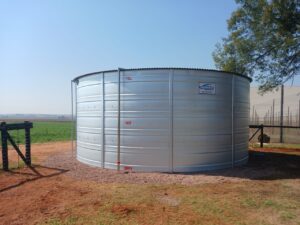
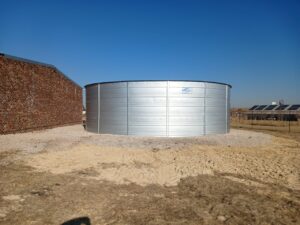
Our Aluzinc® coated steel provides superior resistance to “white rust” and atmospheric corrosion. For food plants, this means a lifespan of over 40 years without the need for toxic repainting or chemical treatments that could compromise the air quality of the facility.
3. Dual-Purpose Storage: Production vs. Fire Safety
Many food production plants face a unique challenge: they require massive volumes of water for high-pressure cleaning and processing, but they also need a dedicated reserve for their fire sprinkler systems.
Rainbow Reservoirs specializes in dual-purpose tank configurations. By utilizing specialized valve systems and internal suction heights, we can provide a single, high-capacity tank that services your daily production needs while strictly “locking away” the mandatory fire reserve required for ASIB compliance.
4. Scalability for Growing Brands
The food industry is fast-moving. A facility that processes 10 tons a week today may need to process 50 tons next year. Our modular “flat-pack” design allows for:
- Fast Installation: Minimizing downtime during plant upgrades.
- Flexible Footprints: We can build tall, narrow tanks to fit into tight spaces between existing factory buildings.
5. Water Security in a Volatile Climate
With municipal water shedding and infrastructure challenges across South Africa, food production facilities cannot afford “dry” hours. A dedicated Rainbow Reservoir acts as a buffer, ensuring that even if the municipal supply fails, your production lines keep moving and your facility remains protected from fire risk.
Ensure your production never stops. Explore our industrial and food-grade storage solutions at www.rainbowtanks.co.za.